If you’ve ever received a quote with a tolerance you weren’t sure how to interpret – or had parts that didn’t fit because an important tolerance was never clearly specified – you’re not alone.
Tolerances can have a big impact on how a part fits, how easily it can be manufactured, and ultimately how much it costs. A tolerance that is tighter than necessary can add machining, inspection, and rework costs without providing any real benefit.
The goal isn’t to specify the tightest tolerance possible. It’s to specify the tolerance your finished assembly actually needs.
What Is a Tolerance?
A tolerance is the amount a dimension is allowed to vary from the specified size.
For example, a 12.000″ dimension with a ±0.005″ tolerance means the finished part can measure anywhere from 11.995″ to 12.005″.
That small range may seem insignificant, but tighter tolerances generally require more careful manufacturing and inspection. Depending on the part and process, that can mean additional machine time, more inspections, and a higher risk of scrap or rework.
That’s why it’s important to use tight tolerances where they matter – and avoid paying for them where they don’t.
Realistic Tolerances by Fabrication Process
Every fabrication process has its own capabilities. As a general starting point, you might see tolerances in these ranges:
| Process | Typical Commercial Tolerance |
|---|---|
| Laser cutting (flat dimensions) | ±0.005″ |
| CNC turret punching | ±0.005″ |
| CNC press brake (bending) | ±0.005″ on critical dimensions |
| Welding | ±0.030″ and up |
| Assembly/hardware insertion | Depends on the part stack-up |
These numbers are general guidelines, not guarantees. Material, part size, geometry, equipment, and the specific manufacturing process can all affect the final result.
One important thing to remember is that cutting and bending are generally easier to control than welding.
Trying to hold a welded assembly to the same tolerance as a laser-cut component can add significant cost—or simply be unrealistic for the process.
Good design for manufacturability (DFM) takes these differences into account from the beginning.
Cutting Tolerances
Laser cutting and CNC turret punching can both produce accurate flat patterns when the right equipment and process controls are used.
For many sheet metal applications, a fiber laser is a practical choice because it can produce complex profiles without requiring dedicated tooling. It can also be cost-effective for lower-volume and highly customized parts.
Turret punching can make more sense for higher-volume work, particularly when the part includes features such as louvers, forms, countersinks, or other punched details that can be incorporated into the blanking process.
Regardless of which process you choose, the flat blank is the starting point for everything that follows.
If the blank is inaccurate, that error can carry through bending, welding, and final assembly.
Bending Tolerances: Where Things Get More Complicated
Bending sheet metal isn’t quite as simple as putting a line on a drawing and expecting the material to follow it exactly.
When sheet metal is bent, the material stretches and springs back. The amount of springback can vary depending on the material, thickness, bend radius, bend angle, tooling, and other factors.
Several things can affect the final dimension:
- Material thickness: Sheet thickness can vary slightly, which can affect the resulting bend.
- Bend radius and angle: Different materials and bend conditions produce different amounts of springback.
- Part size: A long flange can be more difficult to control than a small tab.
- Material type: Different grades of steel, aluminum, and stainless steel behave differently during forming.
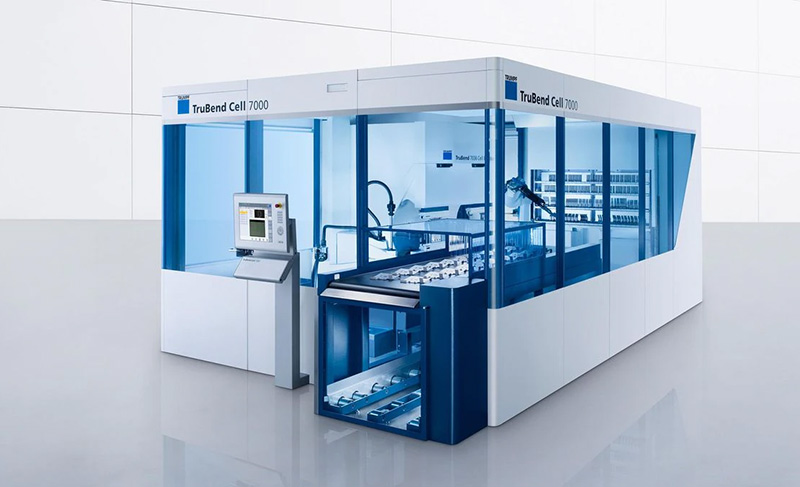
Modern CNC press brakes and properly calibrated back gauges can provide very good repeatability. Critical dimensions may be held to approximately ±0.005″ under suitable conditions.
However, that doesn’t mean every dimension on every bent part should automatically be given a ±0.005″ tolerance.
The better approach is to identify the dimensions that actually affect the fit or function of the finished assembly and apply tighter tolerances to those areas.
Welding Tolerances
Welding is a different challenge altogether.
The heat from welding can cause material to expand and contract, resulting in distortion and shrinkage. Because of this, welded assemblies generally require more generous tolerances than laser-cut or formed components.
A tolerance such as ±0.030″ or more may be appropriate for certain weldment dimensions, depending on the size and design of the assembly.
For critical mounting surfaces, holes, or interfaces, additional steps may be necessary. These might include careful fixturing, post-weld machining, or measuring the assembly after welding.
Robotic welding can improve consistency from one part to the next, but consistency doesn’t necessarily mean the part will be exactly at the nominal dimension shown on the drawing.
If a particular interface is critical, it should be designed and inspected with the welding process in mind.
Quality Systems Matter, Too
A tolerance on a drawing only has value if the manufacturer has a reliable way to verify it.
When you’re evaluating a fabrication partner, it’s worth asking how critical dimensions are measured and documented.
A well-controlled quality system may include:
- Coordinate measuring machines (CMMs) and calibrated inspection equipment
- In-process inspections rather than relying only on a final inspection
- First article inspection (FAI) reports for new or critical parts
- Material traceability back to the applicable material lot
- ISO 9001-certified quality management systems with documented and repeatable procedures
The specific inspection equipment and process should match the requirements of the part.
If a manufacturer is expected to hold a tight tolerance, it should also have the equipment, procedures, and trained personnel needed to verify that tolerance.
How Tolerances Affect Cost
The tighter the tolerance, the more attention a part may require throughout the manufacturing process.
That can mean additional setup time, slower production, more frequent inspections, increased scrap, or additional machining and rework.
You can often reduce cost without compromising the function of the part by following a few simple principles:
1. Tighten only the dimensions that matter
If a mounting hole, mating surface, or critical interface needs a tight tolerance, specify it.
There’s usually little benefit in applying the same tight tolerance to dimensions that don’t affect fit or function.
2. Use a common datum
Whenever possible, reference critical dimensions from a common datum rather than stacking several dimensions together.
This can help minimize accumulated dimensional variation.
3. Plan around welding
Don’t expect the welding process to maintain the same precision as cutting or forming.
If a critical interface must be highly accurate, consider how it will be located, fixtured, measured, or machined after welding.
4. Work with your fabricator
A good fabricator should be willing to review your drawings and point out tolerances that may be unnecessarily difficult or expensive to manufacture.
That’s one of the benefits of a DFM review: potential problems can be identified before production begins rather than after parts have already been made.
The Bottom Line
Tolerances aren’t just numbers that belong on a drawing. They’re part of the overall design and manufacturing strategy.
The right tolerance is the one that gives your assembly the fit and function it needs while still being practical to manufacture.
Understanding what each fabrication process can realistically achieve—and communicating which dimensions are truly critical—can help prevent unnecessary costs, rework, and production delays.
At HFI Manufacturing, we hold ±0.005″ on laser cutting and CNC press brake forming for applicable parts and requirements, supported by an ISO 9001-certified quality system, CMM inspection, and first article reporting.
Our engineers can also review your drawings for manufacturability before production begins, helping identify potential tolerance and fabrication issues early.
Send your drawings for a DFM review or call (630) 293-9300 to discuss your project and tolerance requirements.